Manufacturing
How a Glass Encoder Disc Is Made: From Glass to Finished Disc
A glass encoder disc goes through more than ten process steps: cleaning, chrome coating, resist coating, exposure, development, etching, resist strip, cutting, edge grinding, inspection and packaging. This article walks the whole flow and explains what each step solves and what hidden defects it leaves in the disc if done poorly.
A glass encoder disc looks like nothing more than a thin piece of glass printed with a ring of black lines. But that ring may contain thousands of lines, each only tens of microns or even a few microns wide, with clean edges, complete opacity and concentricity with the centre bore. Such a thing is not just “printed”; it is built up step by step through more than a dozen processes.
Three stages: film, pattern, shape
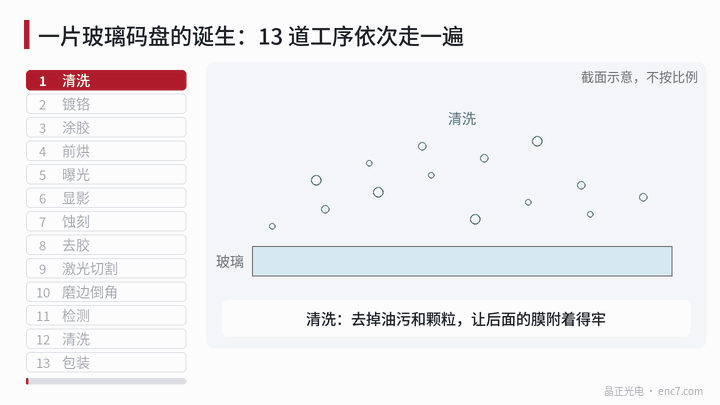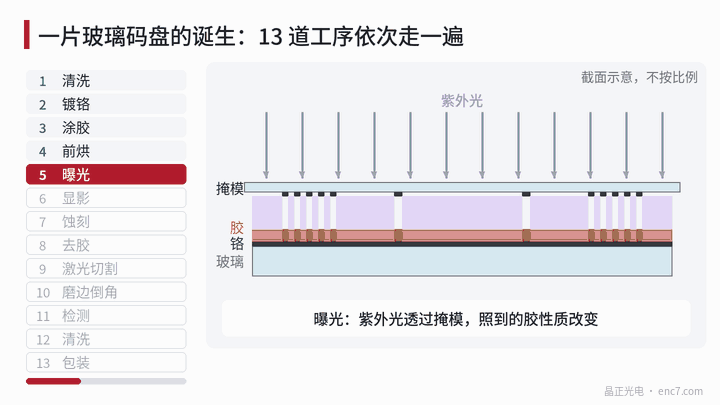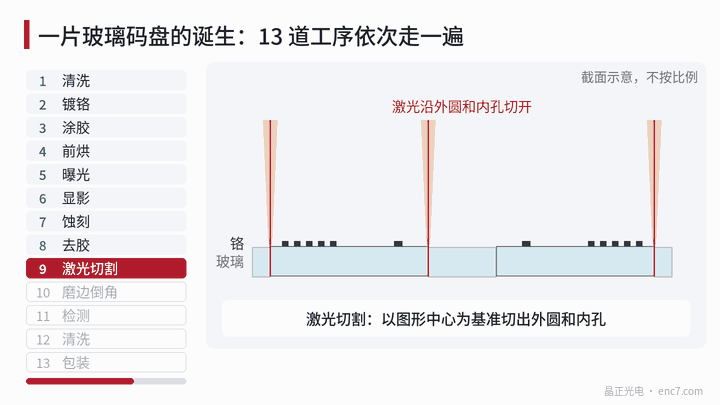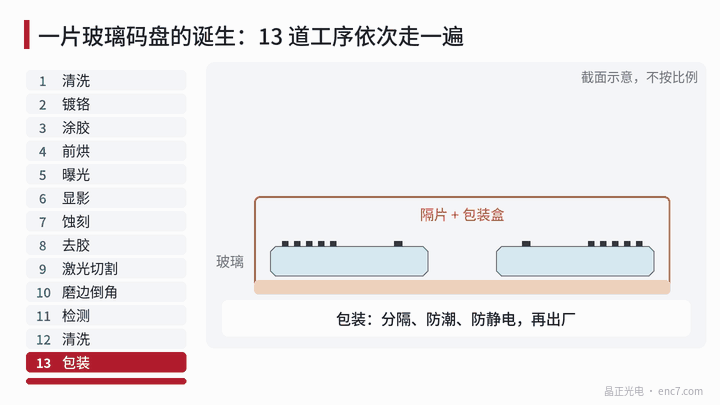
Broken down, the whole flow is really just three things (Figure 1):
- Make the film: clean the glass and deposit a layer of chrome.
- Make the pattern: “copy” the lines onto the chrome film by photolithography and dissolve the unwanted chrome.
- Make the shape and ship: cut the OD and bore, grind the edge, inspect, clean, package.
Let us go through them in that order.
Stage 1: clean glass plus a layer of chrome
Cleaning is the first step and the most easily underestimated. Even a slight oil film or a tiny particle left on the glass means the chrome will not adhere well there, or will leave a pinhole.
Chrome coating is done in vacuum, usually by sputtering or evaporation. The chrome film is generally around 0.1 μm thick — a few hundredths of a hair’s diameter — yet it already blocks light very thoroughly. The “black” parts of the disc are this chrome layer.
Stage 2: copying the pattern by photolithography
Photolithography works like masking tape when painting: first cover the areas to keep with a layer of photoresist, then dissolve the exposed chrome.
- Resist coating: photoresist is dispensed at the centre of the substrate and spun at high speed into a thin, uniform film.
- Pre-bake: heating drives the solvent out of the resist and sets the film.
- Exposure: UV light shines through a mask onto the resist. The mask is the “negative” of the disc pattern.
- Development: with the commonly used positive resist, the exposed parts dissolve in the developer, uncovering the chrome underneath.
- Etching: the etchant dissolves the exposed chrome; chrome covered by resist remains and becomes the lines.
- Resist strip: the remaining resist is stripped, fully revealing the chrome lines.
The final line width is determined jointly by exposure dose, development and etching; if any one of them drifts, line width drifts with it. The same mask is used repeatedly, so batch after batch of discs comes from the same “negative” — the reason lithographed discs are so consistent.
Stage 3: cutting, inspection, shipping
Laser cutting cuts the OD and bore using the pattern centre as the reference. If the cut is off-centre, the line ring and bore are not concentric, producing an eccentricity error once mounted on the shaft: at a read radius of 20 mm, 5 μm of eccentricity corresponds to about 52″ of angular error.
Edge grinding and chamfering removes micro-cracks and sharp corners from the cut, reducing chipping and making the disc better able to withstand assembly forces.
Inspection typically covers line width, eccentricity, optical density and cosmetic defects, using image measurement and automated optical inspection (AOI). Finally the disc is cleaned once more, separated with interleaves, and packaged against moisture and static for shipment.
What each step controls
| Step | Main purpose | Typical result if done poorly |
|---|---|---|
| Cleaning | Surface free of oil and particles | Film peeling, pinholes |
| Chrome coating | Uniform, dense opaque film | Insufficient opacity, pinholes |
| Resist coating, pre-bake | Uniform resist film | Inconsistent line width |
| Exposure, development | Pattern transferred to resist | Line-width deviation, resist residue |
| Etching, resist strip | Pattern transferred to chrome | Residual chrome, broken lines, line-width deviation |
| Cutting, edge grinding | Concentric shape, intact edge | Eccentricity, chipping, cracks |
| Inspection, packaging | Gatekeeping and protection | Defective parts escaping, scratches in transit |
Summary
The steps for a glass disc fall into three stages: film, pattern and shape. Lithography determines line shape and width, cutting determines whether lines and bore are concentric, and cleaning and cleanliness run throughout. Later articles take each step and cover it in detail.
Translated from the ENC7 Chinese technical library (article 0021). Read the Chinese original. Need a disc built to your drawing? Request a quote or see our custom encoder discs.
© Langfang Jingzheng Optoelectronic Technology Co., Ltd. All rights reserved. This article was created with AI assistance.